The 500K Monthly Order
Turning daily output claims into a production calendar that accounts for real working days.

Buy equipment for your normal month, and you may have to turn down the biggest order your sales team has ever landed.
Buy equipment for your biggest month, and six months later you may be staring at a very expensive machine waiting for demand to come back.
Welcome to cannabis production planning.
A 500,000-pre-roll order does not care that your machine only needs one operator. It cares whether 500,000 good, accepted pre-rolls leave the production room before the month does.
That is the part of equipment planning that gets missed. People compare hourly rates, crew sizes and purchase prices as separate numbers. The order sees all of them at once.
Before we get into specific machines, here is the basic calendar math.
If your facility has 22 production days in a month, the daily requirement looks like this:
150,000 accepted pre-rolls requires 6,818 per production day.
200,000 requires 9,091 per day.
500,000 requires 22,727 per day.
For a normal eight-hour shift, that 500K order requires an average of 2,841 accepted pre-rolls every scheduled hour. On a ten-hour schedule, it requires 2,273.
Those are not machine-cycle numbers. They are accepted-output numbers. Startup, breaks, cleaning, material refills, adjustments, changeovers, rejects and rework still have to fit inside the same calendar.
The two formulas worth keeping are pretty simple:
Production days = order volume ÷ finished, accepted output per shift
Direct labor hours = production days × paid shift hours × everyone working inside the measured production boundary
The Bureau of Labor Statistics defines labor productivity as output relative to hours worked. NIST makes the same practical point through overall equipment effectiveness, which accounts for availability, performance and quality. In plain English, speed only helps while the equipment is running and the product coming out is usable.
That may sound obvious. Production floors have a way of making obvious math expensive.
What does 500K look like through the numbers vendors and customers have actually published?
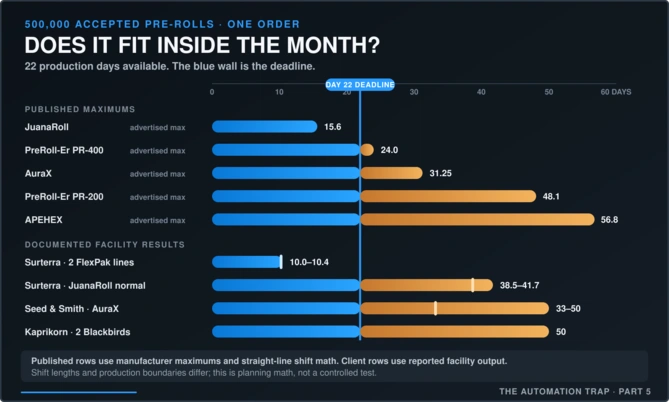
APEHEX advertises up to 1,100 fully weighed, packed and closed cones per hour with one operator. At that published maximum, an eight-hour shift produces 8,800 units. A 500K order takes about 56.8 perfect shifts.
PreRoll-Er publishes up to 1,300 per hour for the PR-200 and 2,600 for the PR-400. Straight-line eight-hour math puts a 500K order at roughly 48.1 shifts on the PR-200 and 24.0 shifts on the PR-400. The larger machine gets close to a 22-day month, but only if it holds the published maximum across every scheduled hour and the resulting units pass the buyer's standards.
AuraX advertises 2,000-plus pre-rolls per hour with one operator. That works out to 16,000-plus over eight uninterrupted hours, or 31.25 shifts for 500K using the 2,000-per-hour figure. A manufacturer-published Seed & Smith case study gives a more complete production boundary: a two-person crew reported 10,000 to 15,000 units per day from full flower through finished pre-rolls in packaging. At that documented rate, 500K takes about 33 to 50 production days.
RollPros publishes approximately 900 joints per hour for the Blackbird and describes 5,000 joints per shift on its main site. In its Kaprikorn case study, two Blackbirds produced about 10,000 rolled joints per day with two machine operators and two additional people grinding material. Final packaging was handled separately. At that reported production rate, 500K takes 50 days before we add the separate packaging boundary.
The eight-channel JuanaRoll is advertised at up to 4,000 cones per hour or 32,000 in an eight-hour shift. On paper, that clears 500K in 15.6 shifts.
On one real production floor, it did not work out that way.
Surterra Wellness, a Parallel (MSO) company, ran an eight-channel JuanaRoll with five to six technicians involved from material prep through approved, packed-and-closed output. David B. told us the team normally produced 12,000 to 13,000 in a scheduled ten-hour shift, with ordinary breaks during the day. Their best reported shift reached 15,000 approved pre-rolls.
At the published 32,000-per-shift maximum, 500K takes 15.6 days. At Surterra's best reported result, it takes 33.3. At the more normal 12,000 to 13,000, it takes roughly 38.5 to 41.7.
Same machine. Same monthly order. Very different production calendar.
That does not mean the JuanaRoll's published number is false. It means a published maximum and one facility's normal accepted output answer different questions.
There are also good examples of full automation doing exactly what it is supposed to do. Doghouse reports that moving to the RollPros Blackbird increased output about four times while cutting pre-roll labor costs roughly 75%. Rebel Spirit reported that its previous 300,000-unit monthly workflow required around 22 pre-roll employees and had become unsustainable before the company changed its production model.
Those are meaningful results. Full automation can be the right answer when the product, material, volume and workflow fit the equipment. The point of this series is not to argue with a good result. It is to make sure the result you are buying is the one your production calendar actually needs.
Surterra gives us a useful comparison because the earlier equipment and the replacement lines were operated inside the same company.
Its best reported JuanaRoll result was 15,000 approved, packed-and-closed pre-rolls in a scheduled ten-hour shift with five to six people. To reach 500K at that best rate would require about 33.3 shifts and approximately 1,667 to 2,000 direct labor hours.
Surterra later moved the work to two FlexPak Max lines, one machine in each line, with four technicians assigned to each. Those eight technicians handle the work from material preparation and feeding through machine operation, mechanical oversight and QA. Final tubing and labeling sit outside both comparisons.
The two lines report 48,000 to 50,000 pre-rolls in a scheduled ten-hour day, with less than 1% rejects. At that rate, 500K takes roughly 10 to 10.4 production days and about 800 to 833 direct labor hours.
At an illustrative $20 per hour, the labor calculation is roughly $33,300 to $40,000 for the previous best-day scenario versus about $16,000 to $16,700 across the two FlexPak lines.
Yes, the faster setup uses more people at the same time. It also finishes the order in about one-third of the calendar time and uses roughly half the total labor hours.

That is why crew size by itself can be such a lousy shortcut. The business pays for hours needed to finish the order, not the number of people visible in one photo.
Surterra's result belongs to Surterra. Another facility may produce the same volume with fewer people, while another may produce less with more. Material, training, floor layout, quality standards and workflow all matter. The useful part is the method: count everyone inside the same production boundary, count what passed, and measure how long the order occupied the calendar.
Now suppose the order is not 500K. Suppose it is 150K, which will be more realistic for plenty of brands.
This is where production velocity starts changing what labor can do elsewhere in the building.
Modern Distribution reports approximately 20,000 packed-and-closed pre-rolls per day from one FlexPak with a two-person core crew after its initial calibration period. That puts a 150K run at about 7.5 production days.
With two machines and four core operators, Modern established a normal 40,000-unit day and reported a best day near 47,000. At the normal rate, 150K takes 3.75 days. At the reported peak, it takes about 3.2.
Markie D. explained what happened to the rest of the old production crew pretty plainly:
“Two people were on the machine. The other six people were doing other things that make us money.”
That is an important distinction. A productive crew does not have to disappear from payroll to create labor savings. Finishing the order sooner lets trained people move to gummies, flower, beverages, vapes, fulfillment or the next paying batch. They become flexible production technicians instead of permanent residents of the pre-roll room.
My Friend Processing gives us a different boundary. Four people operate a two-machine FlexPak line that grinds, sifts, loads, packs, closes, tubes and labels approximately 22,000 retail-ready pre-rolls per day. A 150K order takes about 6.8 production days. Before that workflow, the same four-person crew completed roughly 1,600 to 2,000 finished pre-rolls a day using two knockboxes. At 2,000 a day, 150K would take 75 production days.
That one matters for co-packers and white-label operators. My Friend Processing says roughly 70% of its business is white-label work across about 15 brands. Large orders do not arrive politely spaced across the year. Sometimes three customers decide they need product at the same time because cannabis enjoys keeping operations managers humble.
Rebel Roots Farms (MSO) built capacity in smaller steps. One FlexPak reportedly produced 20,000 to 30,000 packed-and-closed pre-rolls per day with a three- to four-person machine-level crew. That puts 150K at about five to 7.5 production days, and 500K at roughly 16.7 to 25 days on one machine. Rebel Roots eventually expanded to five machines and reported the ability to produce up to 2 million pre-rolls in a month.
Dean S. described why the company added equipment that way:
“We already had the return on investment, so we could immediately invest back into it and get more. That’s why we jumped up to five so quickly.”
These client figures are not interchangeable. Modern and Rebel Roots are reporting packed-and-closed production boundaries. My Friend Processing is reporting retail-ready output through tubing and labeling. Surterra's comparison stops before final tubing and labeling. We are not going to pretend those are identical just because the numbers look tidy in a spreadsheet.
They still show the planning issue clearly.
A producer may need 150K this month, 500K next month after a large co-packing win, and 200K six months later when the market shifts again. Do you turn down the large order? Add overtime and hope the line behaves? Outsource the work and give away margin? Or buy another six-figure system based on one purchase order that may not repeat?
There is no universal answer. But there is a meaningful difference between adding capacity in smaller production cells and making another large, concentrated capital bet.
Current FlexPak pricing starts at $14,350 for a single Max Premium system, while the two-machine Max Enterprise package is $34,800. For comparison, Hefestus currently describes the AuraX at around $230,000, and RollPros notes that fully automated industrial systems can exceed $300,000.
A lower price does not automatically make a machine better. A higher price does not automatically make the order finish sooner. What changes is the amount of capital exposed if demand falls back, the time it takes to add capacity, and how much of the operation depends on one line staying busy.
There is one more question hiding inside that 500,000-unit order:
Five hundred thousand of what?
Capacity belongs to a product format. APEHEX is built around cones. JuanaRoll fills cones. The standard Blackbird rolls straight joints, while RollPros offers a separate Blackbird XXL for larger blunt formats. PreRoll-Er supports different cone and tube-style products depending on the model and tooling. AuraX supports cones, straight-style papers, blunt wraps and infused products.
FlexPak is split the same practical way: Max is designed for cones, while Edge can run cones, straights and blunts. The right choice depends on what a facility actually sells.
If the next white-label order is 100,000 straight joints and your available capacity is cone-only, you do not have 100,000 units of spare capacity for that job. You have a machine that is free.
A specialized platform can be the smartest choice when the product strategy is focused and stable. A multi-format platform may be worth more when the business lives on co-packing, short runs or changing buyer demand. We will get much deeper into that in Part 8, because flexibility deserves more than one paragraph.
For now, the equipment decision should survive three versions of the future:
- the normal month you can reasonably forecast
- the surge month you would rather not turn away
- and the slower month that usually arrives right after everyone gets comfortable
The best production plan is not the one with the largest hourly number. It is the one that gives you enough capacity to say yes without forcing you to bet that the order lasts forever.
A machine can win the demo and still lose the month.
Part 6 is next: The Production Bottleneck. We are going to look at why the fastest machine in the room can spend half its day waiting on the process beside it.
“A machine can win the demo and still lose the month.”
See the real numbers on a FlexPak line.
The FlexPak Max and Edge deliver up to 49,248 packed-and-closed pre-rolls per shift with a 2–3 person crew. USA-built, no mandatory service contract, lifetime technical support.