Cannabis Material Variability
How moisture, grind, density, stems, fines and infusion can change the entire production day.

Some mornings a pre-roll machine runs like it has something to prove.
Then the next batch hits the hopper and suddenly everybody is looking for the Allen keys.
Same crew. Same SKU. Same settings. Different flower.
This is the part of pre-roll automation that is hard to appreciate from a demo video. Cannabis is not a clean, uniform industrial input. One batch can be dry and light. The next can be dense, sticky and full of resin. Change the cultivar, moisture, grind, particle distribution, stem content or infusion and you may change how that material feeds, meters, packs, closes and burns.
The machine did not change.
The material changed the job.

That matters more now because the pre-roll category is moving toward products that are harder to standardize. According to the 2026 State of the Pre-Roll Market Report, 65.4% of surveyed producers sell infused pre-rolls and another 11.8% plan to launch them. Infused products generated roughly $1.68 billion in 2025 and posted 27.8% unit growth.
The same report found that 68.4% of infused producers mix flower and concentrate before packing. Another 35.7% combine kief and flower inside the cone. Those are not minor recipe changes. They can change the way material moves through the entire production process.
This is basic materials handling, not cannabis folklore. Research across powder and granular processing shows that moisture, particle size, particle shape, surface properties and environmental humidity all affect flow. Increase cohesion and irregularity and material becomes more likely to bridge, clump or stop moving consistently through a hopper or feed path.
Cannabis adds a few more variables because it is an agricultural product. Published postharvest research shows that genetics, growing conditions, harvest timing, drying and storage all affect the condition of the finished flower. By the time that flower reaches a pre-roll room, the production team is not dealing with a single standardized ingredient. It is dealing with a moving target.
The equipment manufacturers acknowledge this in their own specifications.
RollPros recommends 10% to 12% moisture and a coarse, fluffy grind for the Blackbird. PreRoll-Er recommends starting with a medium or medium-coarse grind, then says the ideal grind depends on humidity, density and biomass type. APEHEX says its standard system can run infused flower, but limits that claim to distillate or diamonds at no more than 18% of flower weight and recommends a separate system for heavier infusions.
That is not a gotcha. It is actually useful information.
Every production system has a material window where it performs best. The important question is whether that window covers the products your company makes now, and the products sales may ask you to make six months from now.
Dan P. at Perpetual learned how expensive that gap can become.
Perpetual had invested in a RollPros Blackbird and sent Dan and two team members to Washington for training. The expectation was roughly 4,000 to 5,000 joints per day. Once the machine was installed, the team found that the finished quality depended heavily on very precise mill settings.
Dan told us that when the grind moved outside that narrow window, the finished joints became loose and flower could fall from the ends. Perpetual had previously been selling roughly 120,000 to 140,000 pre-rolls per month. During the Blackbird period, Dan said monthly sales fell to roughly 35,000 to 40,000.
Since switching to FlexPak, Perpetual has worked its way back to roughly 140,000 pre-rolls produced and sold per month, with sales continuing to climb month over month. The constraint has moved away from pre-roll production. Dan says the bigger issue now is getting enough prepared material to keep up with the growth, and the company has had to reallocate some of its flower from other products to support the rising pre-roll demand.
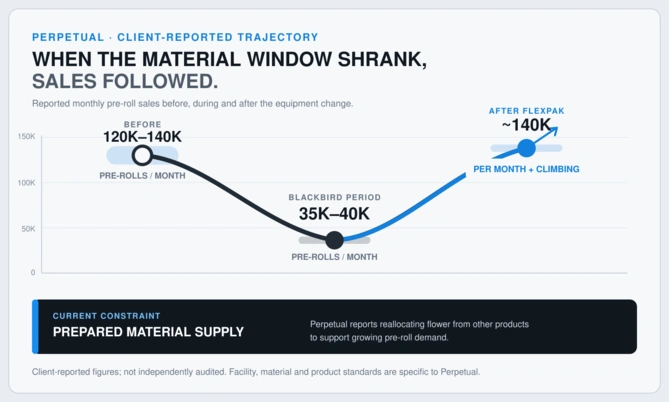
That is Perpetual’s experience with its machine, crew, material and product standards. It is not a claim that every Blackbird produces the same result. RollPros specifically markets the Blackbird around fresh, sticky flower, and plenty of operators may have a different experience.
But it does show why “runs cannabis” is far too broad to be useful.
Runs which cannabis?
At what grind? At what moisture? With how much kief or concentrate? At what finished weight? And how much adjustment is needed when any of those things change?
The issue became even clearer when Perpetual wanted to produce 0.5-gram and 1-gram infused pre-rolls. Dan said those products could not be run successfully on its previous Blackbird setup. Changing products on the automated equipment also meant working through settings, adjustments and recalibration.
After moving the work to FlexPak, his description was pretty simple:
“This machine works extremely well with infused material.”
Perpetual now uses the system for 0.5-gram pre-rolls, 1-gram pre-rolls, 1-gram distillate- and terpene-infused pre-rolls and 0.5-gram infused two-packs.
When the team moves from a 1-gram infused product to a 0.5-gram format, Dan reports that the change takes approximately ten minutes.
“With this, I change a tray. That’s it.”
FlexPak does not make material variability disappear. Nothing does.
The flower still has to be prepared properly. The team still has to watch fill quality, weight and compression. A new batch may still require an adjustment. The difference in Perpetual’s operation is that those changes no longer require the team to rebuild a complicated machine recipe every time the product changes.
We have seen the same basic issue on our own production floor. A dry, evenly milled batch can move quickly and pack consistently. A sticky batch with too many fines may need a different handling rhythm. A batch with stems or uneven particle sizes can create paper damage, weight variation and rework no matter whose logo is on the machine.
The 2026 industry survey puts numbers behind that problem. It found that 63.8% of producers now use a sifter and another 9.5% plan to add one. Producers specifically identified inconsistent moisture as a cause of loading difficulty. Filling problems were also the leading source of rework: 32.7% cited inconsistent fill weight and another 32.7% cited pre-rolls packed too tightly or too loosely.
That means more than 65% of reported rework came from the step most affected by how material meters and packs.
Grinding everything finer is not a universal fix either. Fines may move and compact differently than larger particles, while oversized or jagged pieces can interfere with even filling and damage papers. The same survey found that 63.8% of producers sift specifically to improve particle consistency and remove stems or irregular pieces before packing.
An anonymous operator discussing APEHEX in a public industry forum made a similar point from the floor. They said automated production took considerable trial and error and required material at a lower moisture level than the less automated methods they had used. Another operator in the same discussion described taking months to reach even 80% of the advertised rate on an APEHEX while working through operating and utilization problems.
Those accounts are anonymous, so we are treating them as operator experiences, not verified performance data. But they describe a very familiar pattern: the machine may be mechanically capable of the rate, while the usable material window determines how often the line can actually stay there.
That is why a serious equipment evaluation needs a material matrix, not one successful demonstration.
At minimum, document:
- The cultivars and blends that make up most of your volume
- Actual moisture content and water activity by batch
- Grind size and the amount of fines, stems and oversized particles
- Bulk density after grinding and sifting
- Standard flower versus kief, distillate, diamonds, rosin or other infusions
- Infusion percentage by weight
- Target weights and finished format
- Packed-and-closed output for each material type
- Accepted output after weight, appearance, airflow and burn standards
- Adjustment, cleaning and rework time between batches
Moisture content and water activity should also be tracked separately. They describe different things. Moisture content measures how much water is present. Water activity measures how available that water is for microbial growth and chemical activity. The United States Pharmacopeia’s cannabis expert panel specifically recommended water activity as the more appropriate control for microbial risk in cannabis inflorescence.
Neither number alone tells you whether a pre-roll will pack or burn well. They do give you a repeatable way to understand why one lot behaved differently from another instead of blaming the machine, the operator or the weather based on whoever is standing closest.
Then run the equipment against the ugly part of your production calendar.
Use the sticky cultivar that gives the prep team trouble. Include the infused SKU sales wants to grow. Test the half-gram and the full gram. Track what happens after the first clean batch, after material has been sitting in the room and after the equipment needs to change from one product to the next.
Cannabis cannot legally be carried across state lines for a vendor demo. So that testing needs to happen inside your state, in your own facility or at a licensed operator who can show you comparable production firsthand. If a live material test is not possible, ask for documented production data on material that genuinely resembles yours, including the preparation method and the rejects or rework left out of the accepted number.
The goal is not to find a machine that claims to run everything. That sentence has almost no production value.
The goal is to understand the operating range, how much work it takes to stay inside it and what happens to accepted output when your material moves outside it.
Full automation can work extremely well when the input is controlled, the recipes are stable and the product mix fits the machine. Semi-automated equipment still needs disciplined material preparation and quality control. Neither approach gets a free pass from the flower.
Before you buy, ask one more question after “How fast does it run?”
How many versions of our material can it run well without turning the production day into a science project?
Part 8 is next: Format and SKU Flexibility. Because even if a machine handles the flower, you still need to know what papers, weights and finished products it can make without rebuilding the line.
See the real numbers on a FlexPak line.
The FlexPak Max and Edge deliver up to 49,248 packed-and-closed pre-rolls per shift with a 2–3 person crew. USA-built, no mandatory service contract, lifetime technical support.